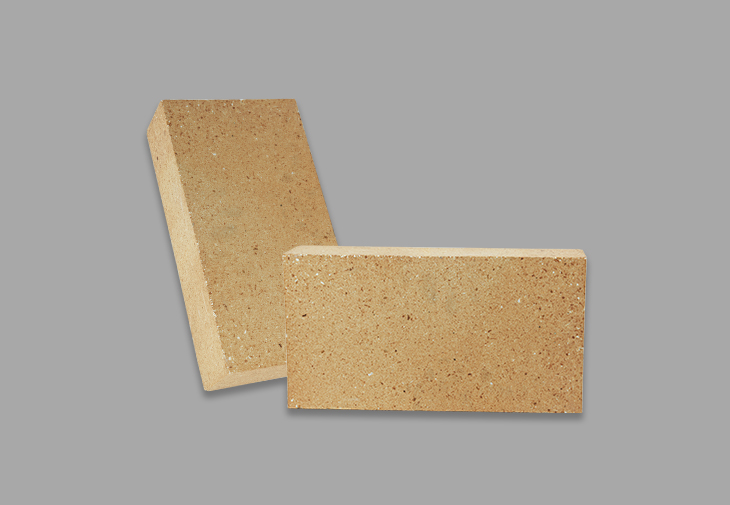


Magnesia bricks are basic refractory products whose performance depends on more than MgO content alone. The manufacturing route and bond system influence the brick’s structure, thermal response, resistance to slag penetration, oxidation sensitivity and handling requirements. The main routes considered in industrial procurement are sintered magnesia brick, fused magnesia brick and unburned or chemical-bonded magnesia brick.
This guide explains how these routes differ and what information a buyer should confirm before ordering. It does not replace the MZ-91, MZ-95 and MZ-97 technical data page. For grade-specific MgO, density, porosity, CCS and RUL values, see the MZ grade and performance guide.
Home ›Magnesia Refractory Bricks ›Magnesia Brick Types
Magnesia Brick Types Guide
| 1. Manufacturing routes | How Magnesia Brick Manufacturing Routes Differ |
| 2. Sintered type | Sintered Magnesia Brick |
| 3. Fused type | Fused Magnesia Brick |
| 4. Unburned type | Unburned / Chemical-Bonded Magnesia Brick |
| 5. Bond and atmosphere | Ceramic-Bonded vs Carbon-Bonded Selection |
| 6. Route comparison | Manufacturing Route Comparison Matrix |
| 7. Furnace use | Typical Furnace Uses |
| 8. Procurement | Basic Procurement Checklist |
| 9. FAQ | Manufacturing and Bond-Type FAQ |
A magnesia brick’s grade and its manufacturing route are related, but they are not the same thing. A grade such as MZ-91, MZ-95 or MZ-97 is used to identify a performance and chemistry level. Sintered, fused and unburned describe how the shaped product is formed, bonded and developed before or during service.
The route affects the internal structure of the brick. It can influence the distribution of magnesia grains, the continuity of the bond phase, the open pathways available for slag penetration, the response to rapid temperature changes and the way the product should be stored, heated and installed. For this reason, two products with similar MgO percentages may still behave differently in a furnace.
Procurement teams should therefore ask two separate questions: first, which performance grade is required for the lining zone; second, which manufacturing and bond route is compatible with the temperature, atmosphere, slag and mechanical duty? This page focuses on the second question. The complete MZ grade data belongs on the MZ-91, MZ-95 and MZ-97 performance page.
Selection principle: Bond type alone does not determine suitability. The final decision requires the furnace atmosphere, slag chemistry, operating temperature, thermal cycle, mechanical load and lining position.

Sintered magnesia brick is produced by preparing selected magnesia raw materials, batching and mixing the formulation, pressing the shape and firing it under a controlled high-temperature schedule. The firing process develops a ceramic-bonded structure and gives the brick its final dimensional and physical characteristics.
For buyers, the important question is not simply whether a product is called “sintered”. The raw material source, MgO purity, secondary oxide limits, grain sizing, forming pressure, firing control and test basis all affect the finished product. The information should be confirmed in the technical data sheet and purchase specification.
Procurement focus
MgO purity, secondary oxides, bulk density, apparent porosity, CCS and RUL.
Potential use
Basic refractory lining zones in cement, glass, lime and metallurgical equipment, subject to the actual service conditions.
Risk to check
Porosity, impurity-related liquid phase, thermal cycling and high-temperature load behaviour.
Sintered does not mean that every product has the same performance. Compare the complete test data, not only the manufacturing name or MgO headline value.
Fused magnesia brick is associated with a route in which magnesia raw material is melted or fused at very high temperature and then solidified or used to form a dense refractory structure. The route can create a different grain and bond relationship from a conventionally sintered brick.
In a quotation review, buyers should confirm the actual product construction, internal integrity, density, porosity, thermal-shock behaviour and machining requirements. A fused route may be considered when the project places a strong emphasis on high density or resistance to a severe service environment, but the route itself is not a universal guarantee of longer service life.
Fused products may also require closer attention to shape, edge condition, cutting and inspection because any defect in a dense, heavy block can affect installation and handling. The required test documents and acceptance criteria should be written into the purchase specification before production.
Where a fused product is being considered for a specific furnace zone, provide the lining drawing, operating temperature, atmosphere, slag information and mechanical load so the grade and construction can be reviewed together.
Unburned magnesia brick is shaped and developed with a chemical or other non-ceramic bonding system rather than receiving the same final high-temperature firing route as a burned brick. The term “chemical-bonded” can cover different formulations, so the actual binder, additives, carbon content and heat-up requirements must be confirmed for the specific product.
The main procurement benefit may be related to the bond system and the way the brick develops during initial heating. The main risks to check are moisture sensitivity, storage conditions, handling strength, oxidation exposure, heat-up schedule and bond stability in the intended atmosphere. An unburned product should never be selected only because its initial quotation is lower or because it carries a familiar MgO grade name.
Before ordering, confirm:
If Highland is quoting an unburned or chemical-bonded product for your project, request the product-specific TDS and handling guidance rather than applying data from a sintered MZ grade.
Ceramic-bonded and carbon-bonded magnesia bricks can serve different duties even when both are described as basic refractories. The bond system affects the way the brick responds to thermal shock, slag, oxygen and the first heat-up.
| Decision Point | Ceramic-Bonded Magnesia Brick | Carbon-Bonded Magnesia Brick |
|---|---|---|
| Main bond | Ceramic bond developed through the specified forming and firing route | Carbon or resin-based bond system, as specified for the product |
| Main purchase focus | MgO purity, density, porosity, CCS and high-temperature load behaviour | Carbon content, antioxidant system, slag compatibility and thermal shock |
| Atmosphere concern | Furnace chemistry and slag interaction remain important | Oxygen exposure and carbon oxidation must be assessed |
| Documents to request | TDS, chemical composition and physical test report | TDS, carbon content, antioxidant and atmosphere guidance |
Bond type alone does not determine suitability. The final selection must consider furnace atmosphere, slag chemistry, temperature, mechanical load, thermal cycling and the exact lining position.

The following matrix is a procurement framework. It does not replace the technical data sheet for a specific grade or the final furnace design review.
| Factor | Sintered | Fused | Unburned / Chemical-Bonded |
|---|---|---|---|
| Main route | Pressed and fired under a controlled schedule | Melted or fused and solidified, as specified | Shaped with a chemical or other specified non-ceramic bond |
| Bond concept | Ceramic bond | Fused crystalline structure | Chemical or resin-related bond, as specified |
| Main strength to evaluate | Balanced basic refractory performance | Density potential and internal structural integrity | Bond behaviour during storage, heat-up and service |
| Main risk to check | Porosity, impurities and firing consistency | Internal integrity, machining and thermal-shock behaviour | Moisture, oxidation, heat-up and bond stability |
| Documents to request | TDS and physical test basis | TDS and structural/physical test basis | TDS, bond system and handling guidance |
Price should not be judged from the manufacturing route alone. Raw material purity, shape, size, production volume, testing requirements, packaging and destination all influence the quotation. Two suppliers using the same route may still offer products with different test bases and service suitability.
The purchase contract should identify the exact product route, grade, chemistry, physical properties, dimensions, tolerances, inspection documents and delivery conditions.
Manufacturing route selection should follow the duty of the lining zone. The examples below are starting points for procurement discussions, not universal replacement rules.
Sintered magnesia products may be evaluated for selected basic refractory zones. Confirm kiln position, feed chemistry, temperature and thermal cycling against the grade TDS.
Compare ceramic-bonded and carbon-bonded requirements by working layer, safety lining, slag line, impact and oxygen exposure. A single route is not suitable for every ladle zone.
Review upper and lower checker courses separately. Temperature profile, alkali vapour, load and thermal cycling determine whether a magnesia grade is appropriate.
Consider dust, abrasion, chemical attack, rotation, thermal cycling and lining geometry before confirming the production route.
For MZ grade-specific selection, visit the MZ magnesia brick performance page.
Before requesting a quotation, prepare the following information. It allows the supplier to match the manufacturing route and bond system to the actual lining duty.
Send your furnace type, lining position, atmosphere, operating temperature, brick drawing, quantity and destination port. The technical team can then help identify the relevant manufacturing route and document requirements before quotation.

Sintered magnesia brick is shaped and fired to develop a ceramic-bonded structure. Fused magnesia is produced through a melting or fusion route that creates a different grain and structural relationship. Compare density, internal integrity, thermal-shock behaviour and the complete TDS rather than selecting by route name alone.
It is a shaped magnesia refractory product that develops strength through a specified chemical or non-ceramic bond rather than the same final firing route as a burned brick. Confirm the binder, additives, storage requirements, heat-up instructions and atmosphere limits for the exact product.
Carbon-bonded magnesia brick may be considered in demanding metallurgical zones where thermal shock and slag resistance are important. The decision must also consider carbon content, antioxidant system, oxygen exposure, slag chemistry, temperature and the exact lining position.
No. MgO content is important, but performance also depends on secondary oxides, grain structure, density, apparent porosity, CCS, RUL, thermal cycling, slag chemistry and atmosphere. Compare the complete technical data and the required furnace duty.
Request the applicable TDS, chemical composition, physical property report, manufacturing or bond route, batch reference, dimensional drawing where applicable, packing list and any inspection documents required by the purchase contract.
Send your furnace type, lining position, operating temperature, atmosphere, slag or feed information, brick drawing, quantity and destination port. We will help identify the route and bond information required for a project quotation.
Related Magnesia Resources